PRODUCTION PROTOCOL

Six-Stage In-House Manufacturing Process

Every stage of production is performed inside our Pithampur works. Components progress through defined verification gates before advancing to subsequent stations.

01
Stage 01

Raw Material Inward Inspection

Inward receipt and inspection of wire coils, sheet metal, stainless steel, and brass rounds.
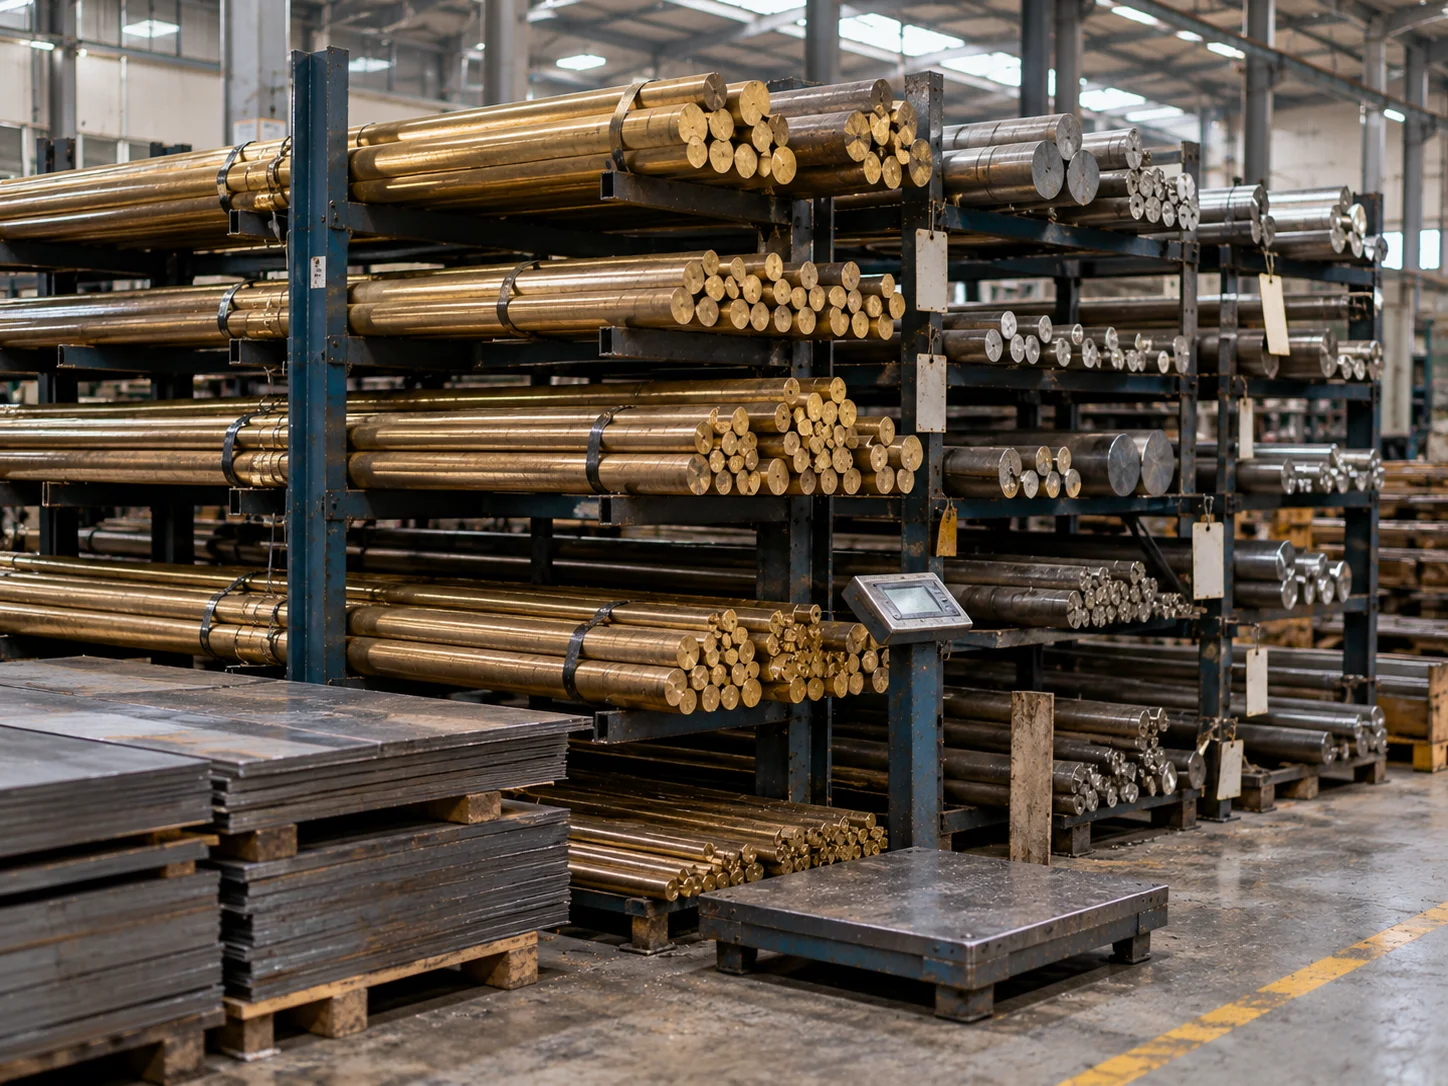
Station / Bays: Raw Material Store and Inward Inspection Bay
Inspection checks: Material grade against mill test certificates, wire diameter, sheet thickness, and surface condition.
Stage output: Verified and accepted raw material lots transferred to machine shop bays.
Raw Material Inward Inspection
02
Stage 02

Machining and Press Stamping

Turning of armature pins and spacer bushes, blanking and forming of brackets and washers, and milling.
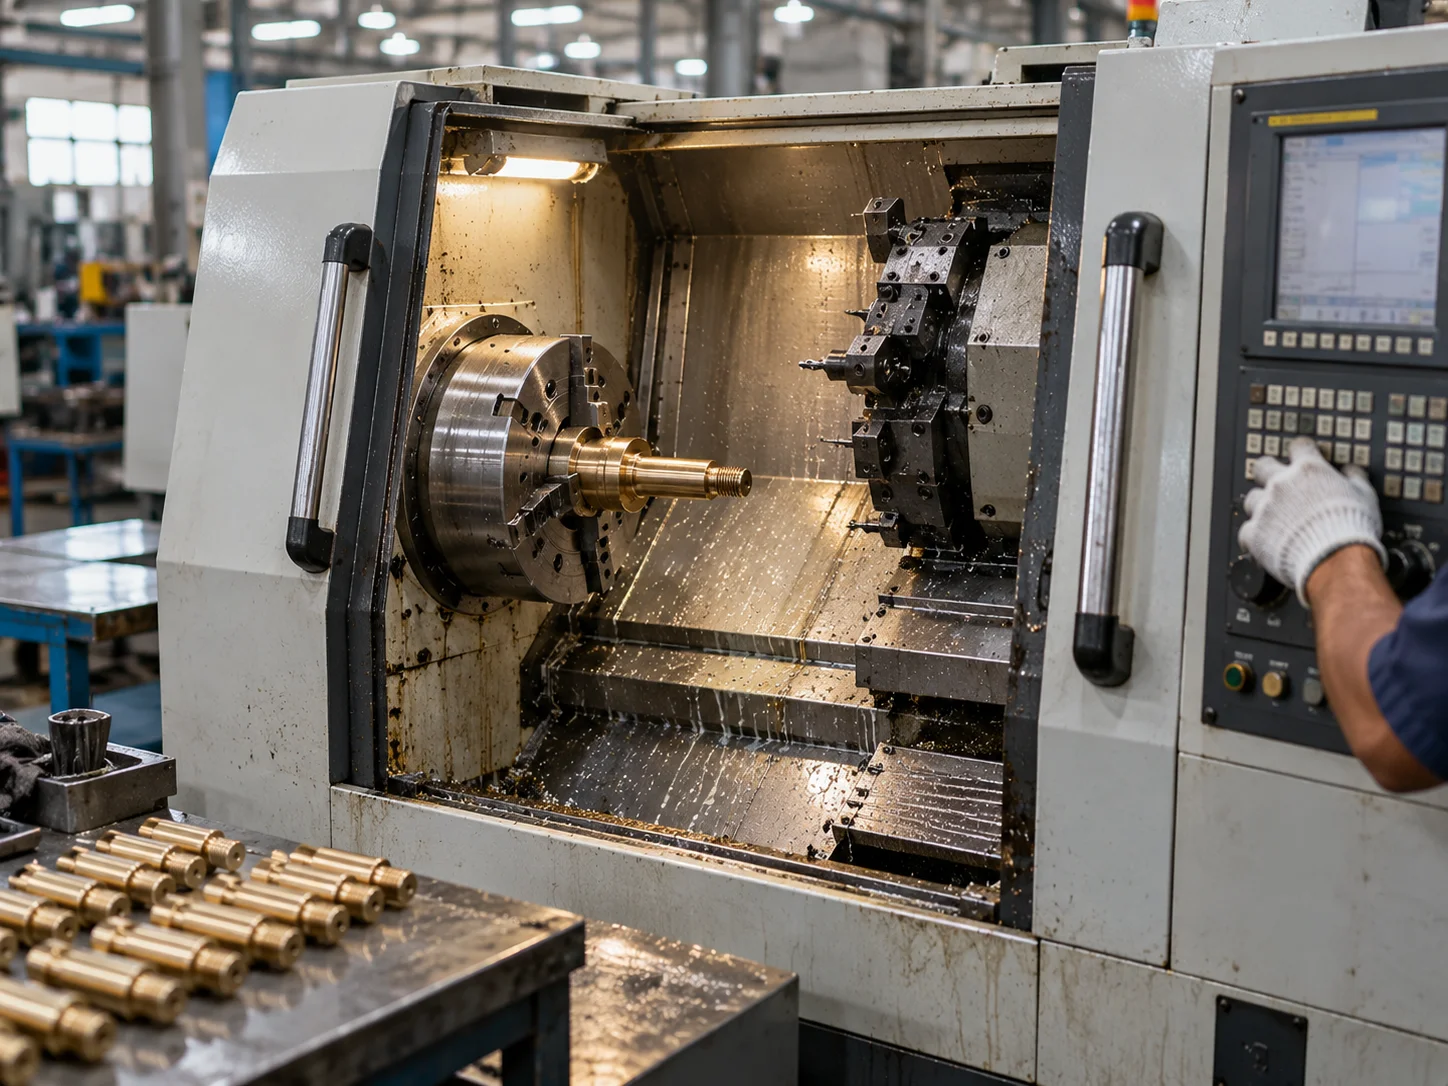
Station / Bays: CNC Lathes, Traub Automatic Lathes, VMC, DRO, and 10 to 75 Ton Presses
Inspection checks: Component dimensions, thread pitch, hole concentricity, bend radii, and deburring against drawings.
Stage output: Machined and stamped component blanks ready for surface finishing.
Machining and Press Stamping
03
Stage 03

In-House Electroplating

In-house electroplating facility applying protective surface finish to relay components. Specifically, relay mounting brackets and metal child parts receive a corrosion-resistant gold-yellow electroplated finish.
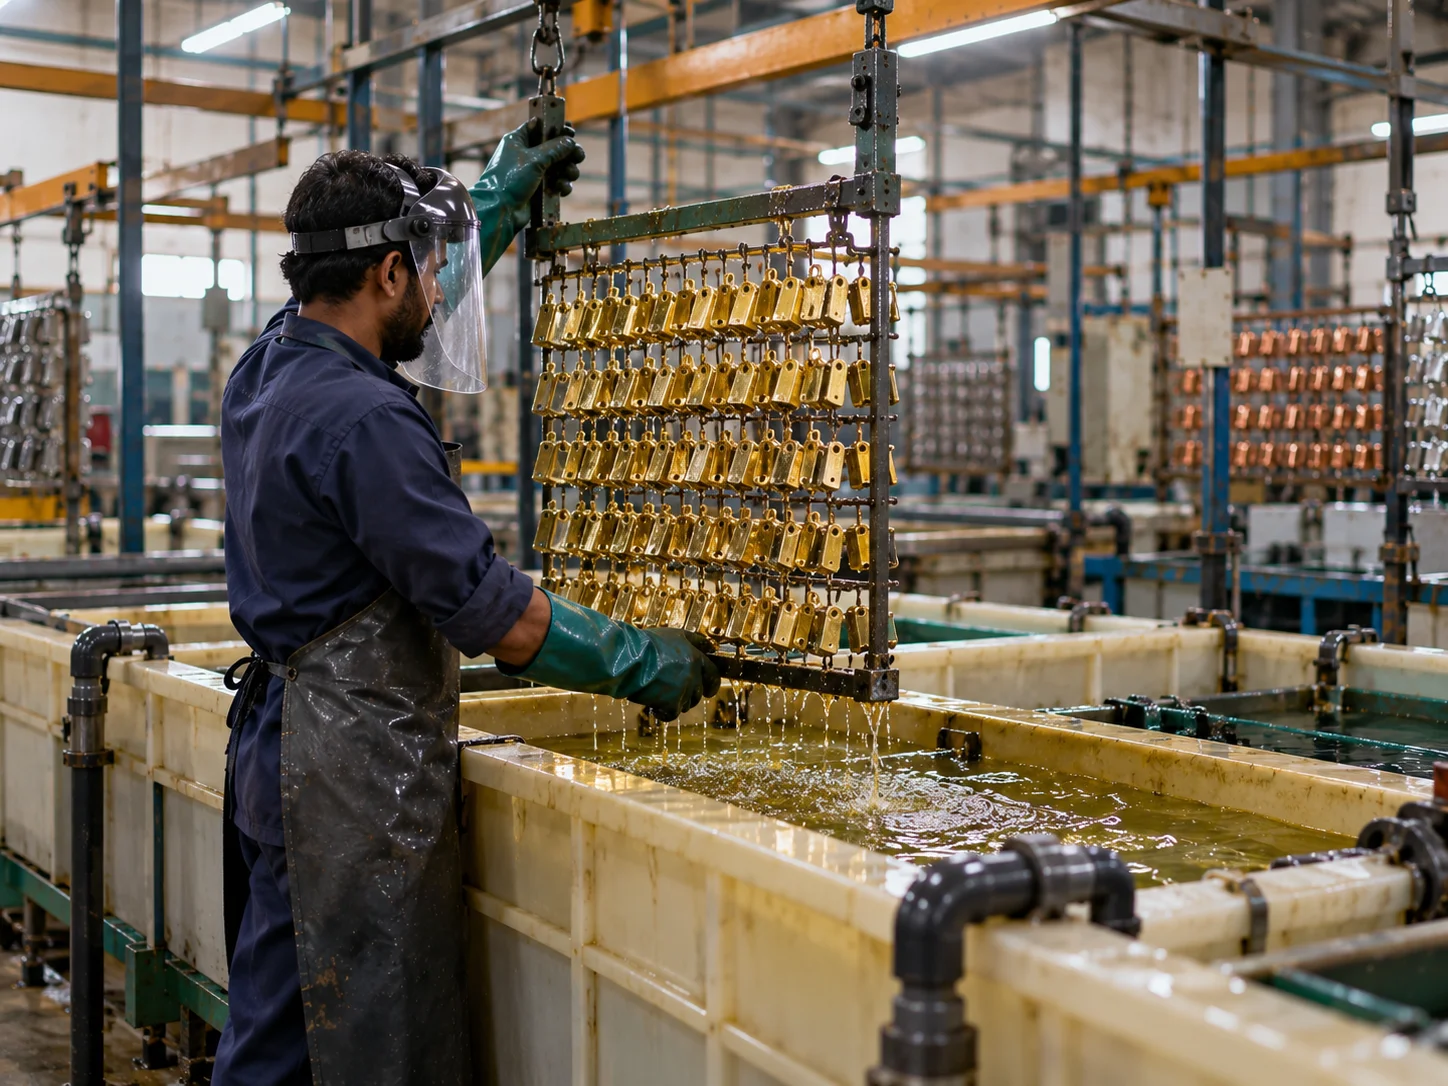
Station / Bays: Electroplating Finishing Bays
Inspection checks: Plating adhesion, coating thickness, and uniform gold-yellow surface coloration.
Stage output: Corrosion-resistant relay brackets and plated child parts.
In-House Electroplating
04
Stage 04

Powder Coating and Vacuum Annealing

Mild steel coach fan guards receive an electrostatic powder coating for a durable, uniform painted finish. Concurrently, electromagnetic components undergo stress relief heat treatment in our in-house vacuum annealing furnace in a controlled vacuum environment.
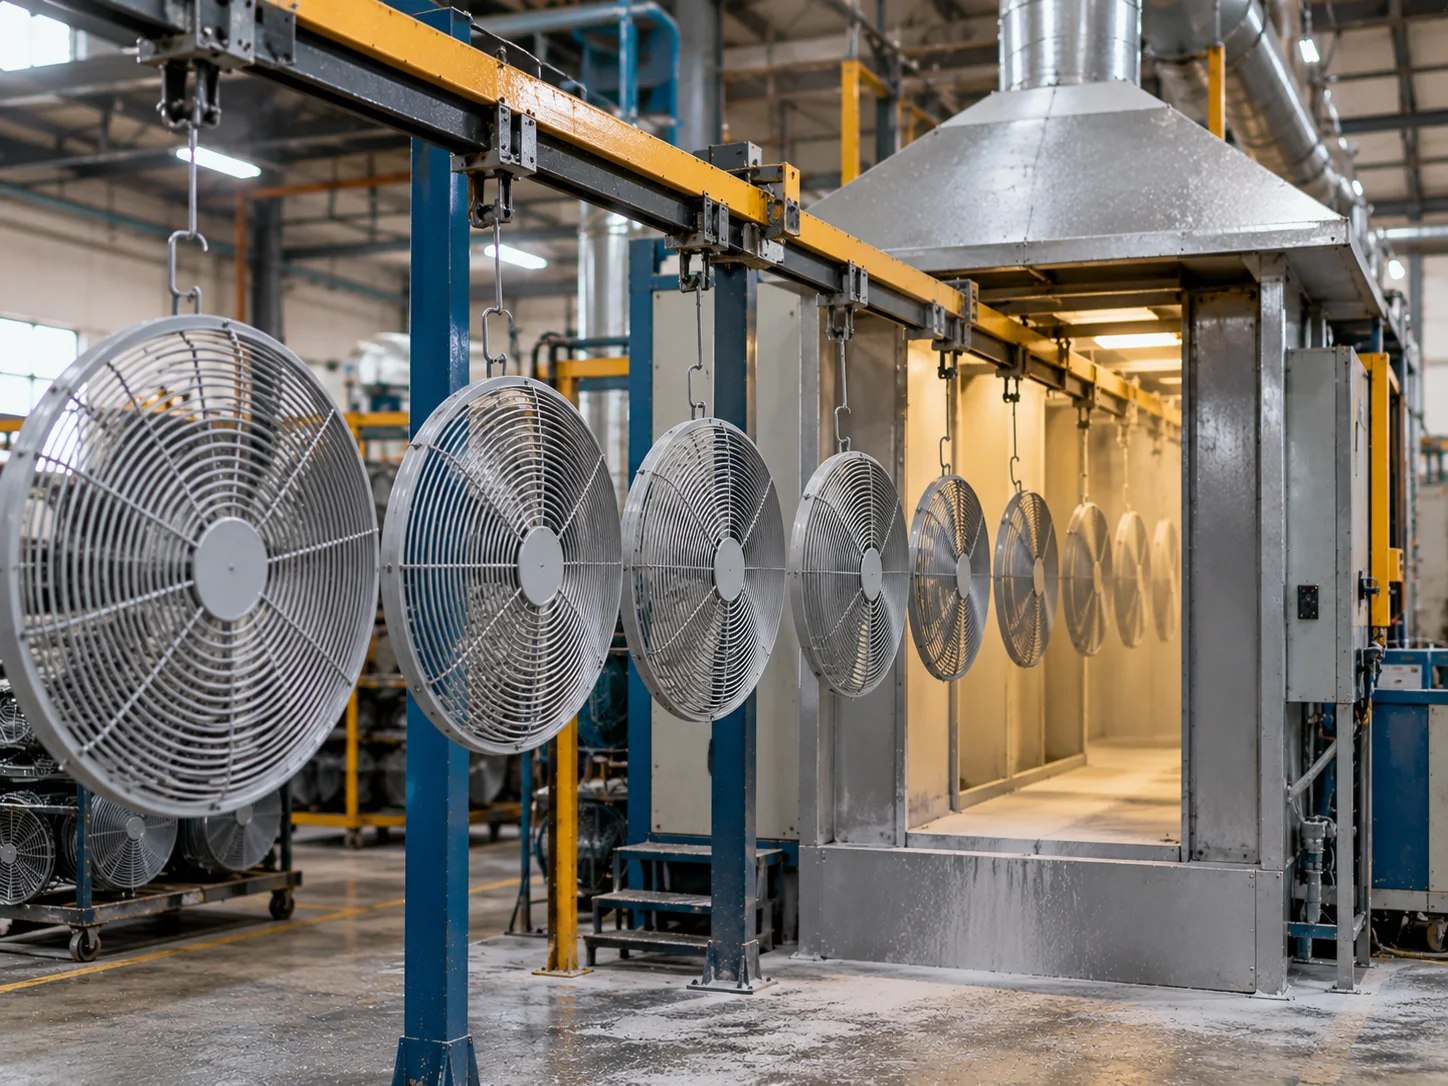
Station / Bays: Electrostatic Powder Coating Booth and Vacuum Furnace Bay
Inspection checks: Powder coating film thickness and adhesion on fan guards; vacuum level and thermal cycle logs for annealed magnetic cores.
Stage output: Durable painted fan guard frames and stress-relieved magnetic components.
Powder Coating and Vacuum Annealing
05
Stage 05

Assembly and Electrical Testing

Precision mechanical assembly of coils, armatures, contacts, and brackets into complete relay assemblies. Each unit undergoes functional testing.
Station / Bays: Clean Relay Assembly Benches and Electrical Test Stations
Inspection checks: Coil resistance measurement (ohms), contact continuity under closed circuits, operate and release mechanical action.
Stage output: Fully functional, verified railway signal relay assemblies and assembled coach fan guards.
Assembly and Electrical Testing
06
Stage 06

Protective Packing and Dispatch

Foam packing of delicate relay assemblies into individual foam slots and batch trays to prevent transit damage. Boxing and labelling of child parts and coach fan guards.
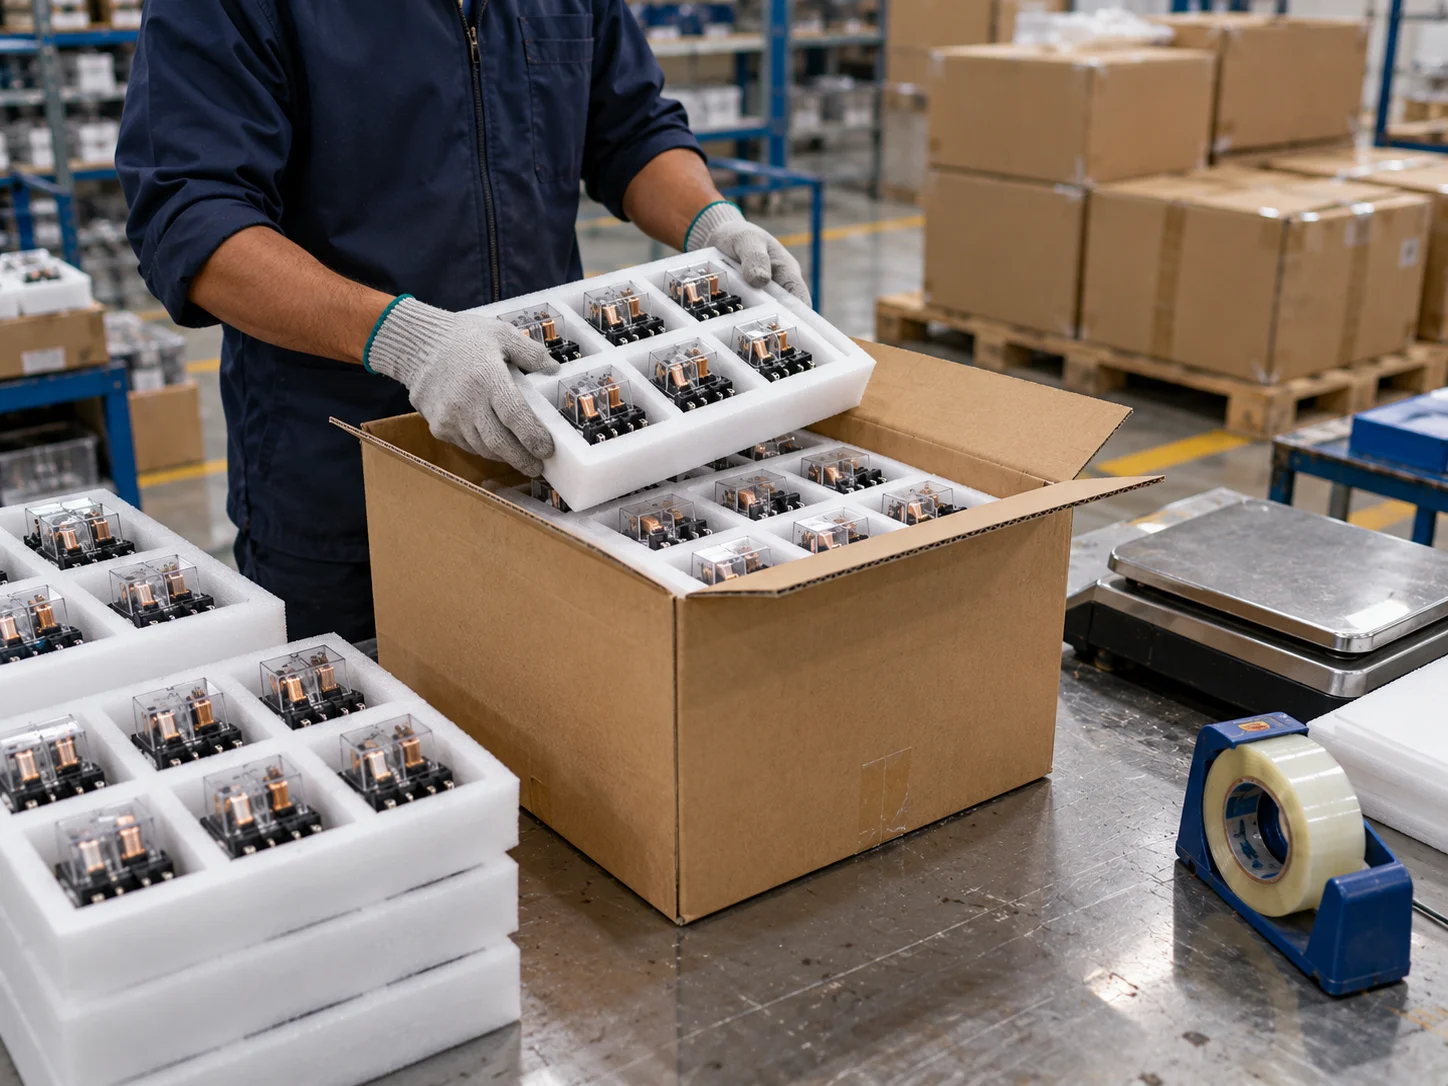
Station / Bays: Packing Station and Final Dispatch Area
Inspection checks: Consignment count against purchase order, visual inspection, foam packing security, and transit carton labelling.
Stage output: Securely foam-packed consignments ready for transport to railway regions.
Protective Packing and Dispatch

Consistent Quality Across Every Production Batch

Our integrated machining, finishing, and testing under one roof ensures end-to-end trace control for railway signalling contractors.